
Views: 0 Author: Site Editor Publish Time: 2026-10-09 Origin: Site


Flange sealing failures rarely stem from catastrophic material breakdown. They usually result from improper compressive stress distribution across the contact area. System vibration and environmental factors rapidly exacerbate this uneven stress. Engineers frequently default to standard dimensions when designing joints. They ignore how the specific edge width of a seal dictates its ability to withstand internal pressure. An incorrect width creates two costly extremes. You either face blowout from insufficient contact area or weeping from inadequate surface pressure.
Specifying the correct edge requires balancing available bolt load, internal system pressure, flange topography, and operating conditions. A narrow profile might crush under heavy torque. A wide profile might fail to seal against micro-imperfections on the metal face. This guide outlines the technical framework for evaluating and defining the exact edge width required for reliable, long-term sealing.
Surface Area Dictates Stress: Increasing the sealing land width decreases the compressive stress for a given bolt load, which can inadvertently cause leaks if the pressure falls below the material's minimum seating stress.
Blowout Resistance vs. Crush Risk: A narrow edge width maximizes sealing pressure but increases the risk of crushing the elastomer or suffering a blowout under high internal pressure.
Flange Topography is the Baseline: The condition, material, and design (raised face vs. flat face) of the mating surfaces dictate the minimum and maximum allowable rubber gasket sealing land width.
Thickness, Width, and Conformability are Interdependent: As a rubber gasket's thickness increases to fill gaps in damaged flanges, its edge width must be proportionally evaluated to prevent lateral extrusion under load.
Vibration and Environmental Isolation: A properly sized sealing land acts as a mechanical dampener for system vibration and a physical barrier against external environmental degradation.
Table of Contents
The sealing land represents the exact radial width making physical contact with the flange faces. You achieve success when this specific area maintains a continuous barrier under maximum operational pressure. It must resist degrading over time. This contact zone dictates the entire mechanical performance of the joint. Fluid dynamics at the boundary layer rely entirely on the surface pressure generated across this radial width. If the surface pressure drops below the fluid's hydrostatic pressure, the fluid migrates across the boundary.
This edge acts as the primary defense against fluid or gas migration. It also serves as a physical shield against external environmental factors. Moisture, chemical washdown, and atmospheric ozone constantly attack the exposed outer perimeter. A properly sized land provides enough sacrificial material to withstand these external attacks while protecting the core sealing boundary. The mechanics of this edge determine how well the elastomer conforms to the microscopic peaks and valleys of the metal flange. You need enough material to fill the flange serrations without overflowing into the pipe bore.
Off-the-shelf dimensions often fail in custom housings or OEM equipment. Standard ASME pipe flange dimensions assume standard operating conditions and standard flange stiffness. Non-standard pressure vessels require shapes and sizes perfectly matched to the mating surfaces. A standard Rubber Gasket might lack the specific radial width needed to handle unique hydrostatic loads. Custom widths ensure the elastomer volume matches the available compressive force. Relying on standard dimensions for specialized applications frequently leads to premature joint failure.
To evaluate the effectiveness of your current sealing land, you must measure three specific operational metrics:
The actual compressed width after full torque application.
The remaining uncompressed thickness at the center of the land.
The visible extrusion past the outer diameter of the flange face.
Gasket sealing land width directly affects compression stress and sealing performance. According to the formula Stress = Force / Area, increasing gasket width reduces compression stress when bolt load remains constant. Proper width selection balances sealing pressure, flange stiffness, and material durability to prevent leakage or gasket damage.
Too Narrow: Excessive compression stress may cause gasket crushing, splitting, or blowout.
Optimal Width: Balanced compression provides reliable sealing without overstressing the rubber.
Too Wide: Insufficient compression stress may prevent proper surface contact, causing fluid leakage.
Edge Width | Compression Stress | Main Risk | Common Symptom |
|---|---|---|---|
Too Narrow | Excessively high | Crushing or blowout | Splitting, sudden leakage |
Optimal | Balanced | Lower risk | Stable, leak-free sealing |
Too Wide | Insufficient | Poor sealing contact | Seepage, gradual leakage |
Engineers should evaluate bolt load, flange rigidity, gasket hardness, and available sealing area together. Uniform gasket width helps distribute compression, but poor flange alignment or insufficient stiffness can still create uneven loading. The final design must provide adequate seating stress without exceeding the gasket's allowable compression limits.
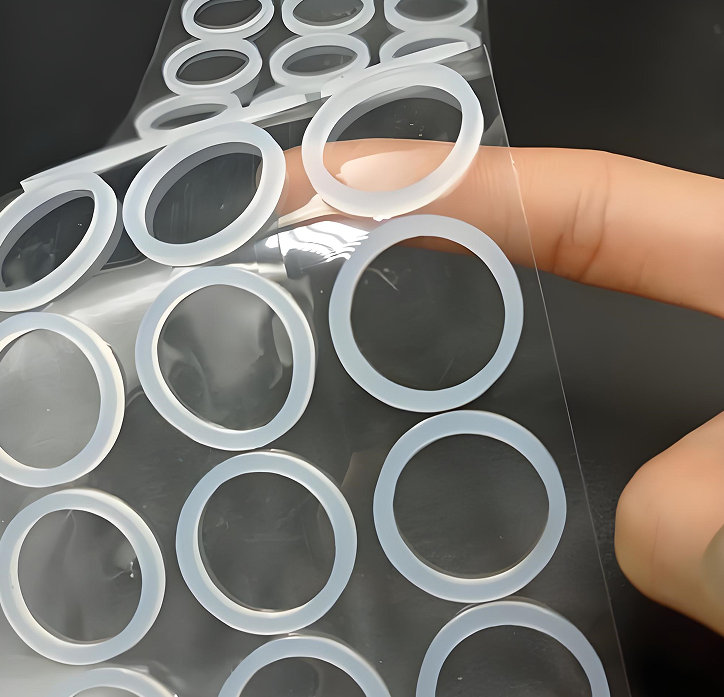
Selecting the correct rubber gasket sealing land width requires balancing flange design, material properties, operating pressure, and mechanical stability. An appropriate width ensures sufficient compression without causing extrusion, deformation, or leakage.
Factor | Design Consideration |
|---|---|
Flange Type | Raised-face and flat-face flanges require different gasket dimensions and load distribution. |
Gasket Thickness | Thicker gaskets may need wider sealing lands to improve stability. |
Operating Pressure | Higher pressures require sufficient sealing stress and blowout resistance. |
Material Hardness | Softer rubber conforms easily but may be more prone to extrusion. |
Vibration & Environment | Dynamic loads and environmental exposure influence gasket durability. |
Key Consideration: Gasket width should be selected together with thickness, hardness, flange rigidity, and available bolt load rather than treating each parameter independently.
Calculating the optimal rubber gasket sealing land width involves evaluating available bolt load, gasket seating stress, and flange geometry. Engineering methods such as ASME BPVC Section VIII, Division 1, Appendix 2 may provide a reference for applicable flange designs.
Determine Operating Pressure: Identify maximum pressure and temperature conditions.
Calculate Available Bolt Load: Evaluate bolt size, grade, and allowable loading.
Identify Required Seating Stress: Refer to gasket material specifications.
Calculate Sealing Area: Use the relationship Area = Force / Required Stress as an initial estimate.
Determine Edge Width: Convert the allowable sealing area into gasket dimensions.
Verify Design: Check compression, extrusion resistance, flange strength, and applicable standards.
The width-to-thickness ratio can serve as an initial design reference for unconfined flat gaskets, but it is not a universal requirement.
Width-to-Thickness Ratio | General Consideration |
|---|---|
Below 2:1 | May present greater instability or extrusion risk |
2:1–3:1 | Possible starting range for preliminary design |
4:1 or Higher | Greater contact area but potentially higher bolt load requirements |
Actual dimensions must be verified against gasket material, pressure, flange geometry, and manufacturer recommendations.
Optimizing gasket width also requires balancing manufacturing cost, standardization, and long-term sealing reliability.
Standard gasket sizes reduce procurement costs, simplify inventory management, and suit many general-purpose applications. Custom gasket widths provide greater design flexibility for unusual flange geometries, demanding pressures, or specific compression requirements.
Die-cutting is cost-effective for repeat production, while waterjet cutting allows rapid prototyping and custom width adjustments without dedicated cutting dies. Manufacturers can validate dimensions through testing before transitioning to high-volume production.
Proper gasket sizing helps maintain consistent compression, reduce leakage, and minimize replacement frequency. Although custom designs may involve additional engineering costs, they can improve reliability and reduce downtime in demanding industrial applications.
Key Takeaway: The optimal sealing land width balances gasket compression, flange strength, material hardness, and manufacturing cost. Final dimensions should be validated through engineering calculations and application-specific testing.
Manufacturing Method | Setup Speed | Dimensional Flexibility | Best Application |
|---|---|---|---|
Standard Die Cutting | Fast (if tooling exists) | Low (fixed to die size) | Standard ASME flanges, high volume |
Custom Die Cutting | Slow (requires new tooling) | High (once built) | Custom OEM parts, high volume |
Waterjet / Flash Cutting | Very Fast | Maximum | Prototyping, low volume, custom widths |
Audit your current flange leakage points immediately to identify patterns of weeping or blowout.
Calculate the exact width-to-thickness ratio for your specific elastomer compound to ensure structural stability.
Implement strict torque control protocols during installation to prevent crushing narrow profiles.
Transition from standard dimensions to application-specific widths for critical joints experiencing chronic failure.
A: The minimum width depends heavily on the material's thickness and durometer. Generally, engineers recommend a width-to-thickness ratio of at least 2:1. For example, a 3mm thick material requires a minimum 6mm width. This ratio prevents the elastomer from rolling, folding, or extruding laterally under compressive load.
A: Thicker materials conform better to damaged or warped flanges but possess lower structural stability. They have a higher tendency to extrude laterally when compressed. Therefore, as thickness increases, the radial width must also increase proportionally to maintain stability and generate sufficient friction against the metal flange.
A: Blowouts occur when the internal hydrostatic pressure exceeds the frictional force holding the seal in place. This failure is usually caused by a sealing land that is too narrow, insufficient compressive stress from the bolts, or using a material that is too thick for the available radial width.
A: Yes. If the width is too large, the available bolt load spreads over too much surface area. This results in compressive stress that is too low to properly seat the elastomer into the flange's micro-imperfections. This low stress leads directly to weeping and uneven pressure distribution.
A: The actual width is the physical cut dimension of the material. The effective seating width is the actual area under compression during operation. Flange rotation, bolt hole placement, and raised face dimensions alter the effective width. Engineers use ASME Appendix 2 formulas to calculate this effective area.
A: Yes. A properly engineered width provides enough mass to dampen mechanical vibrations from pumps and compressors. It also offers a sufficient physical barrier, providing sacrificial material to protect the inner sealing boundary from external environmental degradation like UV exposure, ozone cracking, or chemical washdowns.


